
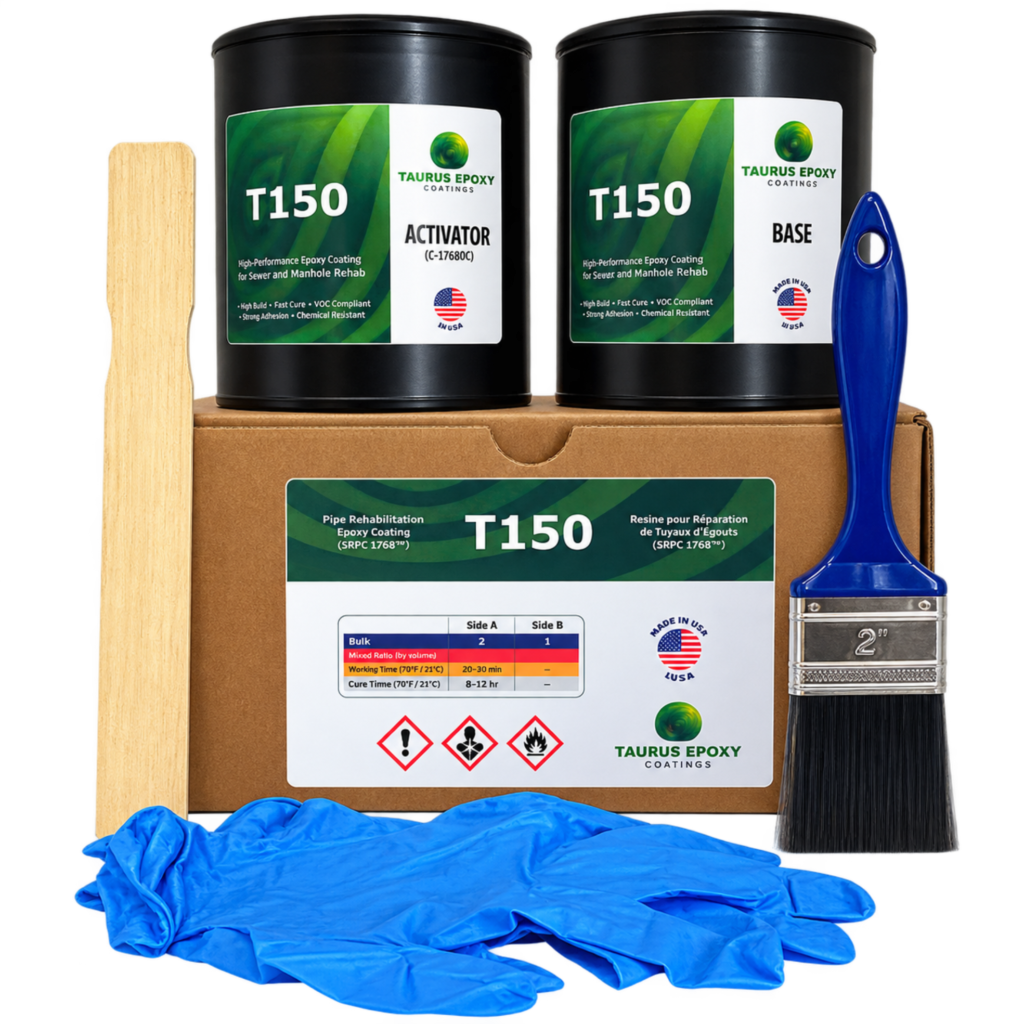
Taurus T150 is a 100% solids, solvent-free epoxy resin formulated for structural reinforcement applications using composite materials. It is designed for use with carbon fiber and fiberglass systems, providing high reliability and excellent performance under a wide range of service conditions. It is suitable for applications exposed to temperatures up to 150°C (302°F).
| Maximum Temperature (Depending on service) | Wet Service | Dry Service | 90°C | 150°C | 194°F | 320°F |
|---|---|---|---|
| Solids by Volume | 100% | ||
| Mixed Density | 1.25 | ||
| Hardness of the Shore D Durometer | (ASTM D 2240) | 85 | |
| Pot Life | 25 min / kg at 72ºF | ||
| Mix Ratio | 2.6:1 by Weight | Base: Activator | |
| Shelf life (unopened containers) | 3 years at 55-95ºF (13-35ºC) | ||
Surface Preparation
Proper surface preparation is critical to the long-term performance of this product. The exact requirements for surface preparation vary with the severity of the application, the expected useful life and the initial conditions of the substrate. All sharp edges and welds shall be roughed to a radius of 3mm (120 thousand) with abrasive disc. The optimal preparation will provide a thoroughly cleaned surface of all contaminants and rough to an angular profile between 75-125 m (3-5 mil). This is normally achieved by initial cleaning and degreasing and then abrasive blasting to near-white metal cleaning, or by mechanical preparation.
Mixing
Mix the activator well in the base with the mixing rod scraping the sides and the bottom of the container. Mix by weight 2.6 parts Base to 1 part of Activator. Mix thoroughly to produce a uniform and without stripes. Never put solvents.
Application Temperature
Keep between 55 and 95°F (17 to 35°C). Substrate: keep between 45 and 105°F (7 to 40°C). The temperature difference of the substrate and material should never exceed 10°F (5°C). The substrate shall be at least 5°F (3°C) above the dew point. Do not apply if the relative humidity exceeds 90%. If necessary, heat the metal before surface preparation using electric heater or heat lamp. Never use gas, oil or kerosene heaters, as they will leave a greasy residue on the
metal surface. For best results, keep all material in the warm zone overnight (75°F+) for easy mixing.
Application
Use a heavy plastic brush or putty knife to apply a minimum thickness of 6 mm. Work the material in the substrate profile to achieve maximum adhesive and remove any trapped air. Contour to correct the shape with putty knife material or plastic applicator. If mold is used or shape, be sure to coat its surface with an agent of release to prevent adhesion of the material.
Cured Time:
| 16°C (60°F) | 25°C (77°F) | 32°C (90°F) | |
|---|---|---|---|
| Tack Free | 4 hours | 2 hours | 1 hour |
| Light Load | 12 hours | 6 hours | 3 hours |
| Overcoat End | 16 hours | 10 hours | 5 hours |
| Full Load | 24 hours | 12 hours | 6 hours |
| Full Chemical | 48 hours | 24 hours | 12 hours |
Clean:Tools should be thoroughly cleaned immediately after use with a strong alkaline detergent.
Safety: Before using any product, review the Safety Data Sheet (SDS) or Safety Data Sheet for your area. Follow standard confined space
entry and work procedures, if applicable.
FDA Compliance: This product complies with FDA regulations: FDA 21 CFR 175.300 and FDA 21 CFR 175.105.
The manufacturer, Taurus Epoxy Inc., makes no express or implied warranties, including warranties of merchantability or fitness for a particular purpose for this product. Under no circumstances shall the manufacturer be liable for incidental, consequential or other damages, breach of warranty, strict liability or any other theory arising from the use of this product. The information and recommendations contained herein are based on the Standard Product and are owned and provided solely for the use of our customers. This information is provided in good faith and is believed to be true and accurate as of the date/version of this document. As the manufacturer has no control over the conditions of use or the application process of the parts using this product, the manufacturer cannot accept responsibility for loss, injury or other damage resulting from the use of the Product or this or any other information provided by the manufacturer. Therefore, no warranties of any kind, express or implied, are made by the manufacturer, Taurus Epoxy Inc., with respect to this, or any, product manufactured by them or any contracted or licensed manufacturer. Taurus Epoxy products do not provide structural integrity or improvements. They are only used to provide protection against corrosion, wear, abrasion and chemical attack on a given substrate and only to the extent provided for in data sheets, data sheets, safety data sheets and any other information provided in writing directly from manufacturers’ technical support.